Our products
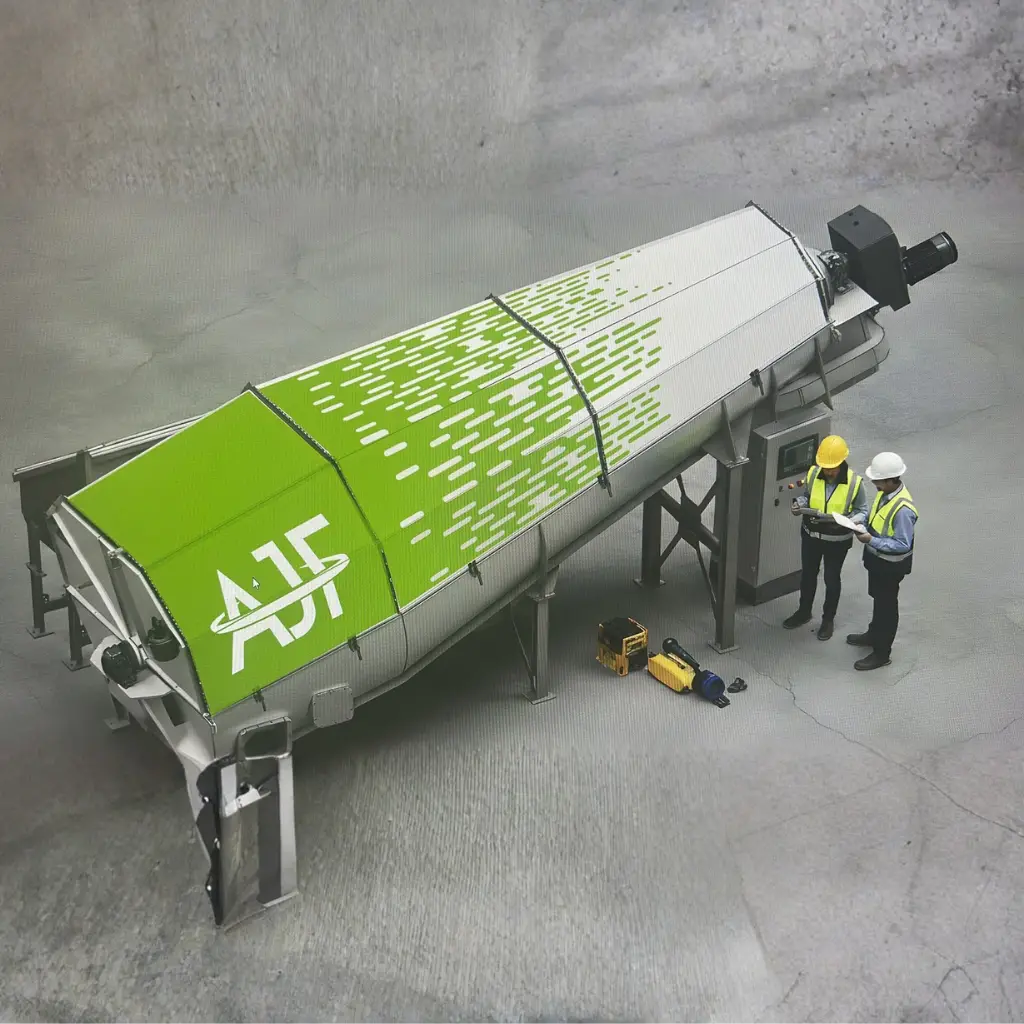
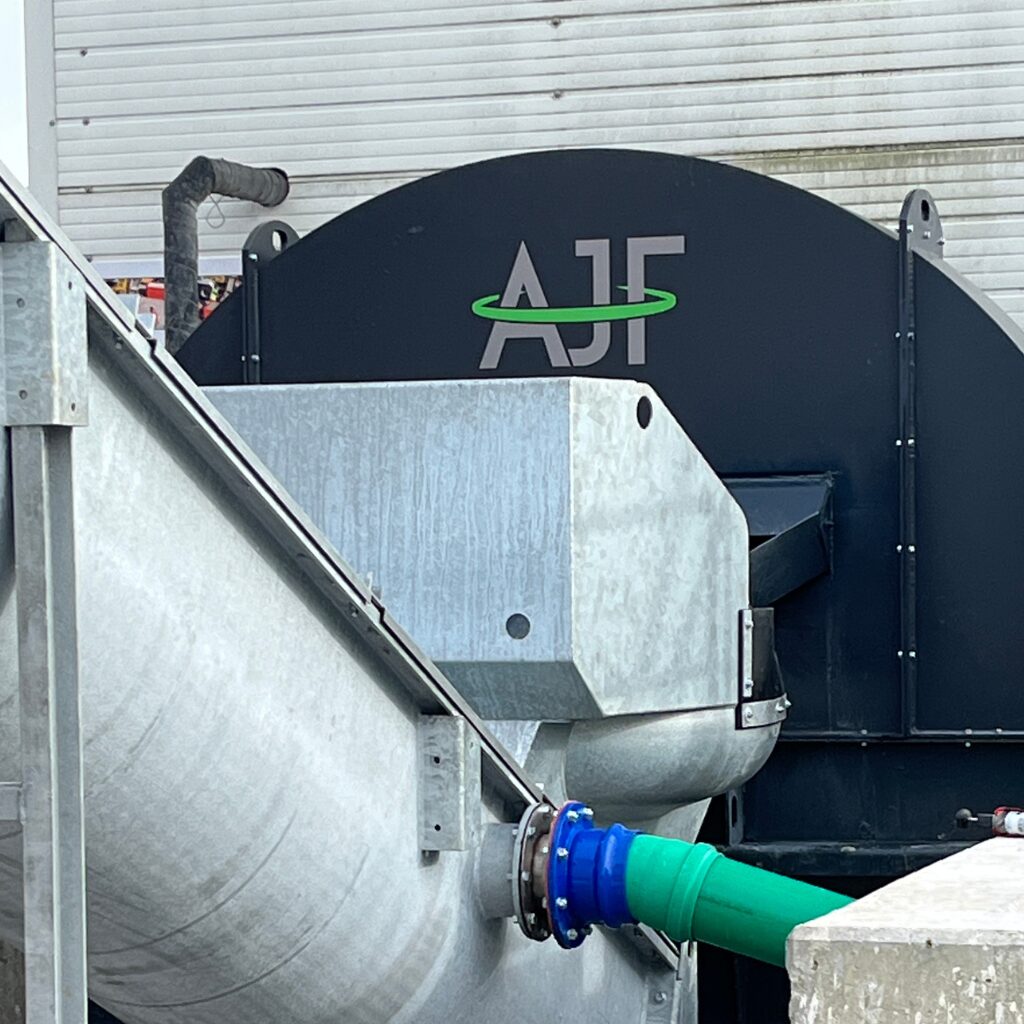
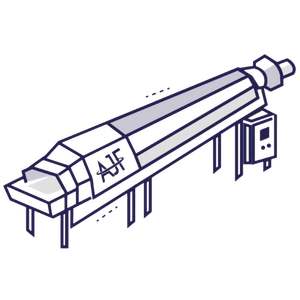
The AJF recycling plant for residual concrete is the innovative answer to the concrete industry’s growing demands for sustainability, cost-effectiveness, and resource conservation.
Whether for ready-mix concrete manufacturers, ready-mix concrete plants, or producers of precast concrete elements, our concrete recycling plant sets new standards in the efficient management of residual concrete and cleaning water.
The reuse of residual water as added water is regulated in DIN EN 1008. Overall, this process enables the reuse of almost all residual concrete.
The process
1
Processing of fresh concrete from mixer trucks or concrete plants
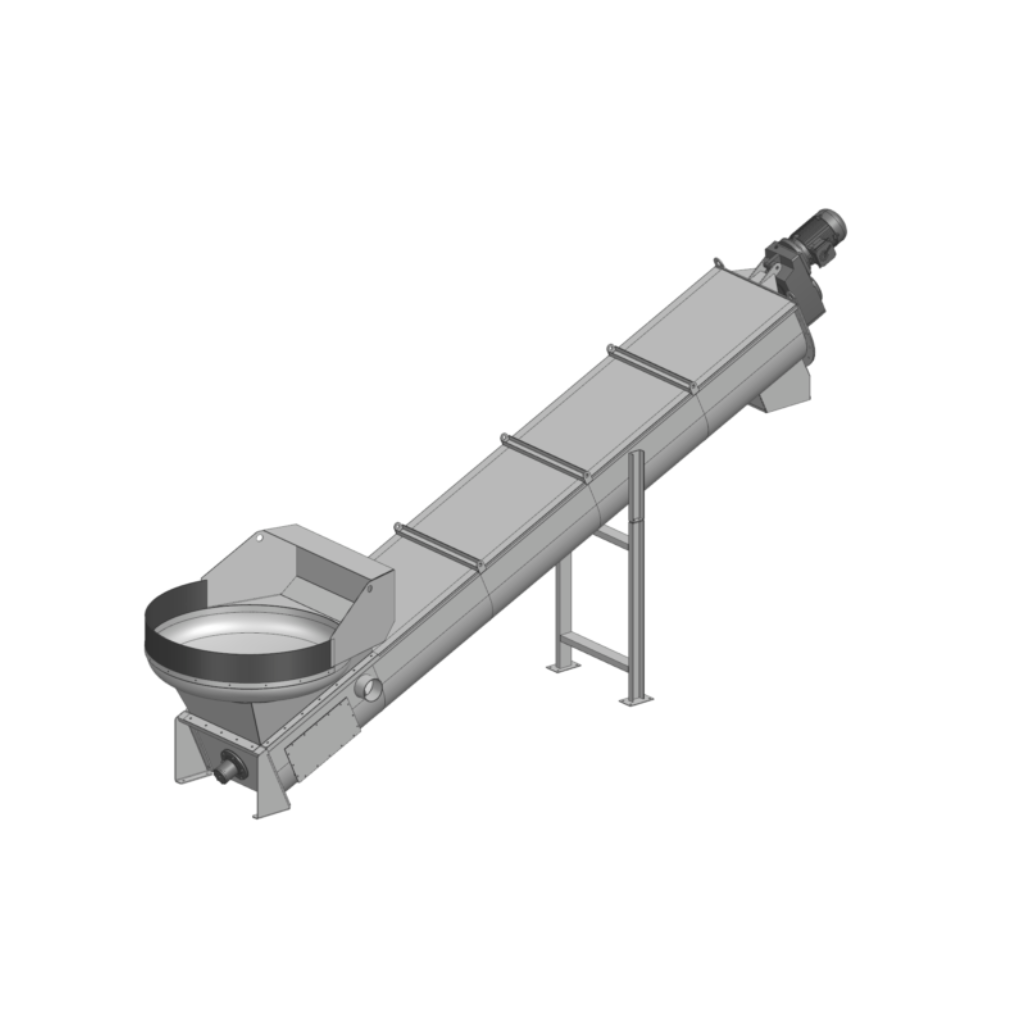
Concrete that comes back from mixer trucks or excess concrete that accumulates in precast plants is poured in liquid form onto the feed table of the recycling plant an diluted. The concrete can then be brought to the required consistency using water via the rinsing arm. The washing speed must be adapted to the respective capacity of the plant.
2
Washing and separation of mixed gravel
Concrete generally consists of the main components aggregate, sand, cement, and water. In the water bath of the recycling plant, the components of the fresh concrete are seperated from the cement paste by stirring and washed accordingly. The washed mixed gravel produced in this way exits at the outlet of the concrete recycling plant. The plant removes all grains larger than 0.2–0.3 mm. The contaminated concrete residual water is separated from the mixed gravel and fed into an agitator tank via the side outlet of the plant. The recycling plant separates the grain sizes between the residual water and the mixed gravel.
3
Mixed gravel as a raw material
The washed mixed gravel obtained in this way is a valuable raw material. It leaves the plant in a free-flowing state and can be reused as an aggregate in many types of concrete. The mixed gravel is discharged into a material container.
4
Treatment of residual concrete water
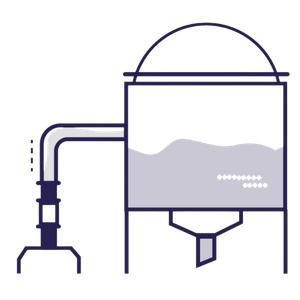
Any residual water or wash water should be collected in the agitator tank. An agitator keeps the fine particles and sediments in constant suspension. The CWAS water treatment system from AJF maintains a constant residual water density in the agitator tank, thus ensuring consistent production conditions and concrete quality.
Advantages of our products
Processing of recycled concrete directly from truck mixers
Cleaning concrete pumps and mixing plants
Separation and recovery of recyclable materials from cleaning water
Integration into existing production processes
AJF’s recycling solutions enable residual concrete and cleaning water to be reused in a resource-efficient manner. The state-of-the-art concrete recycling systems enable valuable materials to be handled sustainably directly at the point of use.
Returnable concrete from construction sites or residues from cleaning mixing plants, truck mixers, and concrete pumps are processed efficiently and in an environmentally friendly manner with the AJF residual concrete recycling plant.
Sustainable use of concrete and water
High-quality workmanship and durability
Reduced disposal and operating costs
Space-saving, flexible design of the concrete recycling screw conveyor
Easy integration into existing systems
Sustainable, economical production